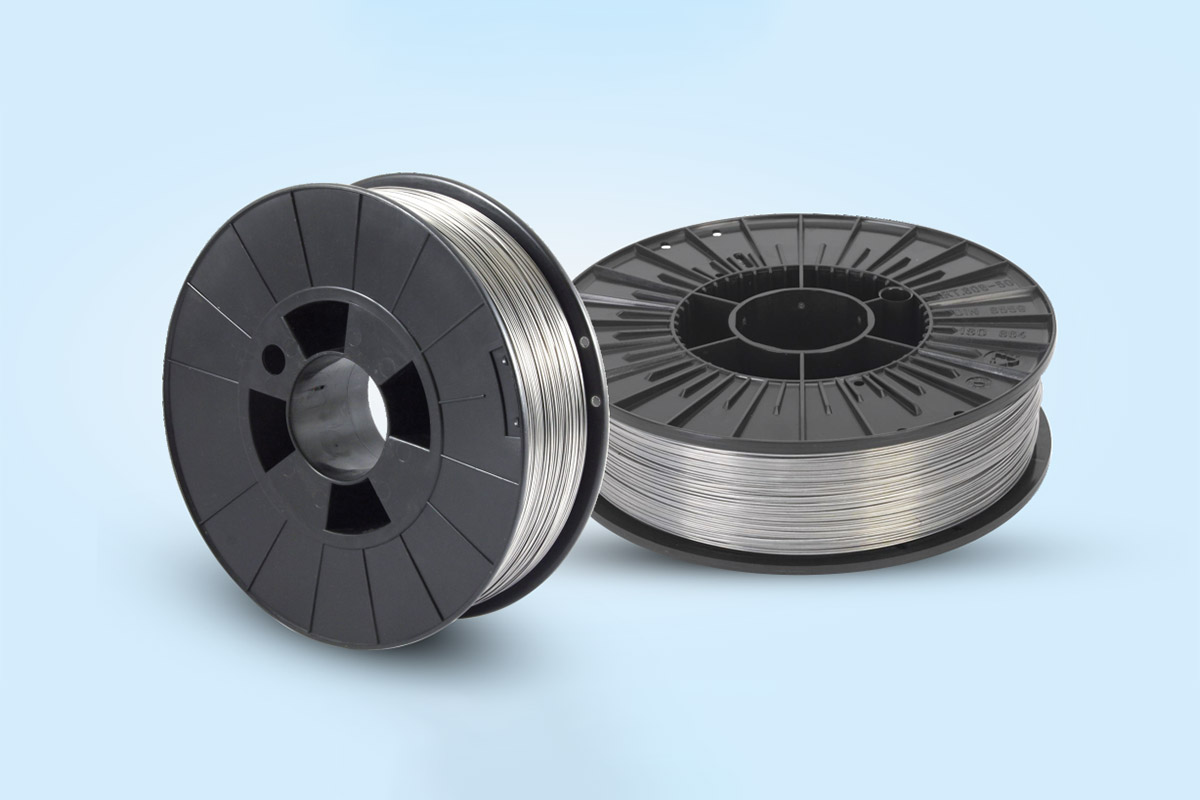
A superior alloy designed especially for extra tough hot and cold work tooling applications. To be used as welded without subsequent heat treatment.
Carver 9580 has exceptional wear characteristics at high temperatures. Ideal for press dies, screw press dies, and impactor dies. It is also used effectively for cold forming applications such as automotive trim sections, forming dies and blanking dies. Machinability is limited to EDM grinding.
For repairs, prepare area to be welded by removing all cracks, heat checks or other defects. Clean area of any slag, scale, rust or drawing compounds. Preheat die blocks and other units where the entire working surface is to be welded to 425º C. On other alloys preheat and post-heat according to the base metal. Maintain temperature during welding. Use the stringer bead technique. Peen the weld when forgeable to relieve stresses. After welding, cool in still air to 150º C to obtain the ultimate grain refinement and uniform hardness in the weld deposit. Post-heat at 550º C for one hour per inch of thickness. Cool in Still air to room temperature.
| SMAW | FCAW | MCW |
|---|---|---|
| DC+ | DC+, 100% CO2 Or 75% Argon-25% CO2 |
DC+, 100% CO2 Or 75% Argon-25% CO2 Or 90% Argon-10% CO2 |
| TECHNICAL DATA | |||||||||
|---|---|---|---|---|---|---|---|---|---|
| Alloy Type | 5% Cr Hot work tool steel | ||||||||
| Hardness | Rockwell C 56-58, as welded | ||||||||
| Available Processes | SMAW, FCAW & MCW | ||||||||
| Class | Hot work tool steel | ||||||||
| Heat Treatment | Use H-12 Procedure | ||||||||
| ELECTRODES | |||||||||
|---|---|---|---|---|---|---|---|---|---|
| SIZE(MM) | 3.15 | 4.00 | 5.00 | ||||||
| AMPS | 120-150 | 160-190 | 200-240 | ||||||
| FLUX CORED WIRES | |||||||||
|---|---|---|---|---|---|---|---|---|---|
| SIZE(MM) | 1.6 | 2.4 | |||||||
| AMPS | 270-320 | 330-370 | |||||||
| METAL CORED WIRES | |||||||||
|---|---|---|---|---|---|---|---|---|---|
| SIZE(MM) | 1.6 | 2.4 | |||||||
| AMPS | 270-320 | 330-370 | |||||||