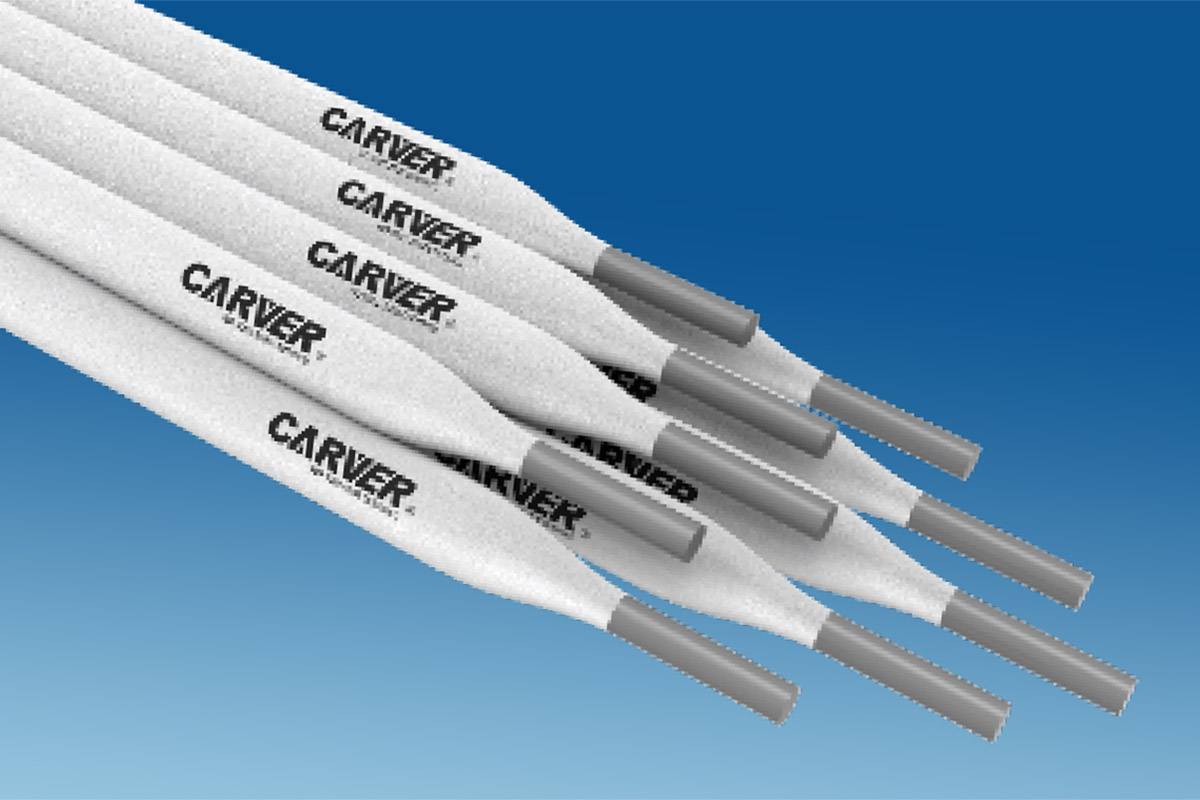
A commercially pure nickel weld deposite is produced which is easily machined, drilled, tapped and field,. Heavy cross sections welding is possible, HAZ is easily machinable, minimum penetration and hence very less dilution.
Carver 9700 is preferred for welding thin sections of cast iron where high dulution occurs and maximum machinability is required as encountered on shy castings and machining errors. CARVER 9700 is also excellent for building up on large castings. Ideal for salvaging foundry castings, gear box and differential housings, glass moulds, Cast iron dies. Best suited for repairing intricate cast iron parts, water pump housings, electric motor bodies, covers, machine frames, and cylinder blocks. It is recommended for joining of carbon steels to all grades of cast iron.
Prepare weld area by beveling and cleaning cracked edges to be joined. Use CARVER chamfer electrodes for all beveling applications. Preheat part to 250°C. Maintain interpass temperature (70°C). Use stringer bead or weaving technique. Peen to relieve stresses. Wrap with thermal blanket and allow casting to cool slowly to room temperature.
| TECHNICAL DATA | |||||||||
|---|---|---|---|---|---|---|---|---|---|
| Alloy Type: | Commercially pure nickel | ||||||||
| Tensile Strength: | 350 N/mm2 | ||||||||
| Machinability: | Excellent | ||||||||
| Hardness: | Rockwell C 19-24 | ||||||||
| ELECTRODES | |||||||||
|---|---|---|---|---|---|---|---|---|---|
| SIZE(MM) | 3.15 | 4.00 | 5.00 | ||||||
| AMPS | 90-110 | 110-130 | 140-170 | ||||||