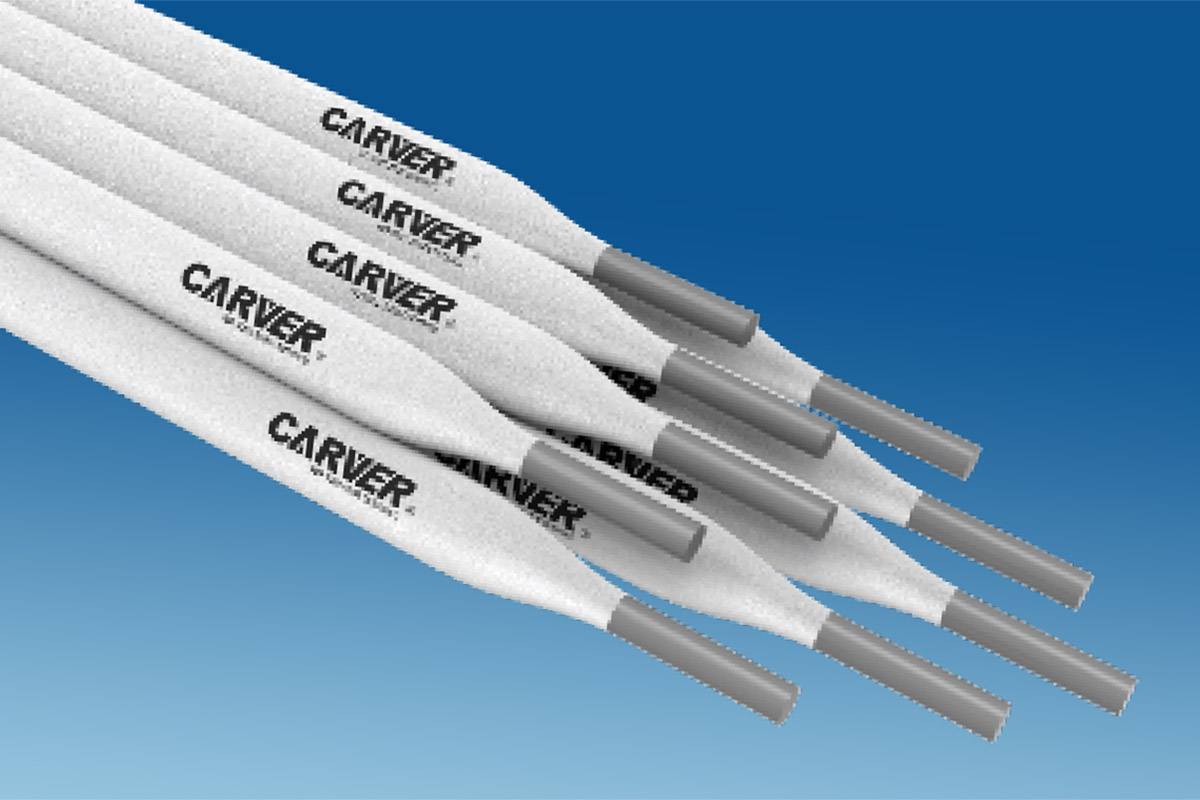
A superior all position welding electrode possessing a unique coating and special alloy core wire that produces a homogeneous, porous-free joint, machinable weld deposit. Deposits are dense and smooth, crack desensitized, resistance to corrosion and heat. These features along with a high tensile, ductility and elongation make CARVER 9880 a versatile electrode for maintenance purposes.
Use for joining cracked die section, high manganese, tool steels, high carbon, low carbon, and stainless steels. Used for hot and cold shears, springs drill shanks, springs, drill shank extensions, heat-treat baskets. It is most suitable for difficult to weld, unknown and unknown and unidentified steels to one another.
Use either AC or DC, reverse polarity. Clean weld area. Bevel heavy sections to be joined. On high alloy tool steels it is advisable to preheat accordingly to the base metal to obtain maximum results. Generally, on other applications preheating is not necessary. Hold a short arc and use stringer beads. Peening will help to relieve stresses. Slag will peel off easily after each pass cools. It is Nonheat treatable weld deposit.
| TECHNICAL DATA | |||||||||
|---|---|---|---|---|---|---|---|---|---|
| Alloy Type: | Nicket-Choromium-Super Strength | ||||||||
| HardTensile Strength: | 800 N/mm2 | ,||||||||
| Elongation: | 24-30% | ||||||||
| Machinability: | Excellent on all base metals | ||||||||
| Hardness: | Rockwell C 20-22 | ||||||||
| ELECTRODES | |||||||||
|---|---|---|---|---|---|---|---|---|---|
| SIZE(MM) | 2.5 | 3.15 | 4.00 | 5.00 | |||||
| AMPS | 50-70 | 70-110 | 100-130 | 150-180 | |||||